In an exciting development for the additive manufacturing industry, Fuji Corporation, a renowned Japanese technology company, has recently formed a strategic partnership with J.A.M.E.S. GmbH, a leading German firm specializing in Additively Manufactured Electronics (AME). This collaboration aims to propel the growth of additive electronics and revolutionize the way electronic devices are manufactured. The partnership brings together Fuji’s innovative electronics 3D printer, FPM-Trinity, and J.A.M.E.S.’s expertise in building an online community dedicated to advancing AME technology.
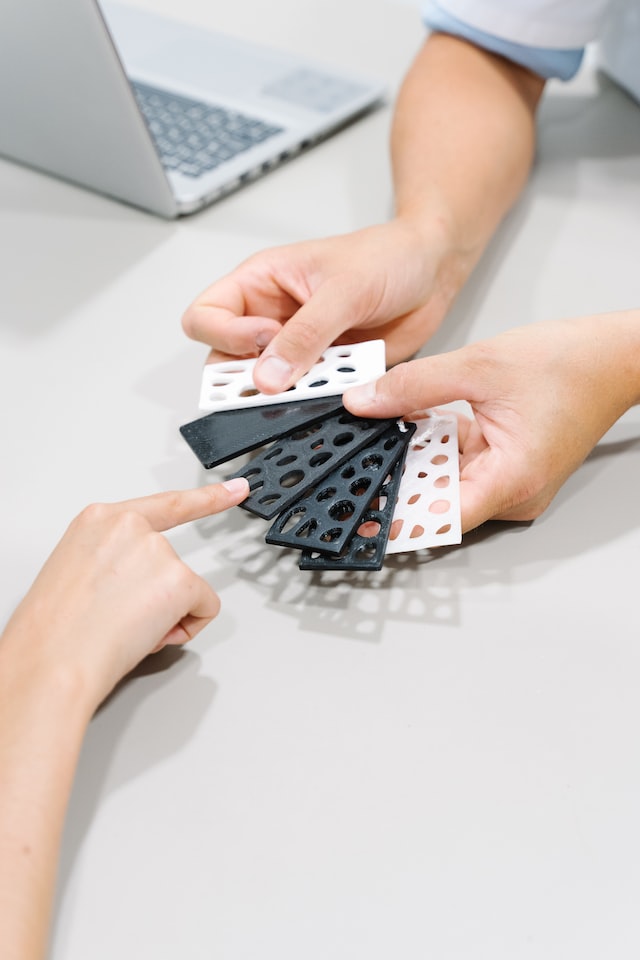
IoT Board Printed with FPM-Trinity Source : Fuji
Fuji’s FPM-Trinity: A Game-Changing Electronics 3D Printer
At the heart of this partnership lies Fuji’s groundbreaking electronics 3D printer, the FPM-Trinity. This unique machine combines resin substrate printing, circuit printing, and component mounting capabilities, allowing for the complete additive manufacturing of electronic devices in a single process. The FPM-Trinity eliminates the need for multiple manufacturing steps, streamlining the production of electronic components and reducing time-to-market.
J.A.M.E.S.: Pioneering AME and Enabling Collaboration
J.A.M.E.S., an abbreviation for “Joint Additively Manufactured Electronics Standarization,” was established with a specific mission to promote the development of AME. The company has created an online community that serves as a hub for manufacturers and users to collaborate, communicate, and share knowledge in real time. By joining forces with Fuji, J.A.M.E.S. aims to explore the full potential of AME and make it a technology accessible to all.
Advantages of the Partnership
Through this partnership, Fuji intends to leverage J.A.M.E.S.’s network to exchange information and enhance the value of its products. The collaboration will provide Fuji with valuable insights from end-users, which can influence the company’s business strategy and future product development. Moreover, the partnership opens doors for Fuji to propose novel ideas and solutions using the FPM-Trinity, driving the adoption of AME across the electronics industry.
IoT Board Printed with FPM-Trinity Source : Fuji
FPM-Trinity’s Key Features and Benefits
The FPM-Trinity offers a range of features that make it a game-changer in the world of additive electronics:
All-in-One Solution: This electronics 3D printer combines resin printing, circuit printing, and parts placement within a single machine, streamlining the manufacturing process.
Direct Digital Printing: FPM-Trinity enables direct printing from CAD data, eliminating the need for additional processes such as mask creation. This feature saves time and increases efficiency.
Rapid Turnaround: With FPM-Trinity, it is possible to go from data input to completion within a single day, significantly reducing production timelines.
3D Form Factor: The FPM-Trinity allows the creation of electronic devices with complex 3D geometries, expanding design possibilities and enabling innovative product development.
Sustainable Manufacturing: By minimizing waste materials and optimizing material usage, the FPM-Trinity contributes to sustainable manufacturing practices.
Future Developments and Impact of AME
Fuji Corporation currently offers a sample manufacturing service utilizing the FPM-Trinity. However, their long-term goal is to release the machine for sale, advancing the development and widespread adoption of additive manufacturing technology. This initiative is expected to address industry challenges such as the rapid growth of the Internet of Things (IoT), the pursuit of sustainability, and the need to shorten product development cycles.
Conventionally, printed circuit boards (PCBs) are manufactured through subtractive processes, involving etching away unnecessary materials. In contrast, AME utilizes 3D printing techniques to selectively apply materials only where required, resulting in minimal material waste and liquid
The decision to insource or outsource additive manufacturing is not simply a comparison between machine price and supplier quotation. It is a capability decision involving application pipeline, utilization, intellectual property, process ownership, qualification, post-processing, inspection and long-term supply risk.
Buy a machine when owning the manufacturing capability creates durable strategic value. Buy parts when external capability delivers the required result with lower total risk.
Three operating models
Model
What remains internal
Best fit
Outsource
Requirements, design authority, supplier management and acceptance
Early adoption, variable demand, specialized processes or limited internal expertise
Hybrid
Application engineering, prototyping or selected builds; external production or post-processing
Organizations building knowledge while managing capital and qualification risk
Insource
Equipment, operators, process control, production data and often post-processing
Strategic IP, stable workload, rapid iteration, controlled qualification or supply-chain need
Many successful programs move through these models over time. Outsourcing can be the fastest way to validate applications. A hybrid model can build internal design and process knowledge. Full insourcing becomes attractive only when the application portfolio, organization and downstream infrastructure are ready.
The first question: what capability are you buying?
An AM machine does not create an industrial capability by itself. A complete capability may require:
Application and DfAM engineering
Build preparation and process engineering
Feedstock storage, handling and traceability
Qualified equipment, software and parameters
Environmental, health and safety controls
Heat treatment, HIP, debinding or sintering
Support removal, machining and surface finishing
Cleaning, metrology, NDT and material testing
Quality systems, data retention and change control
Maintenance, service and spare-parts support
If most of these remain external, the organization may be insourcing a printer while still outsourcing the production system.
When insourcing is strategically attractive
Rapid design–build–test loops
Internal equipment can compress iteration cycles when engineers, operators and test teams work closely. This is valuable for R&D, tooling, repair development and products whose geometry changes frequently.
Sensitive intellectual property
Insourcing can reduce exposure of geometry, parameters and performance data. It does not remove cybersecurity risk; internal access, file transfer and machine networks still need control.
Stable and repeatable demand
A credible internal application pipeline improves equipment utilization and supports operator proficiency. The pipeline should be based on production-ready candidates rather than a long list of parts that are merely printable.
Qualification ownership
Some organizations need direct control of parameters, machine condition, material genealogy and production records. This can justify insourcing when the qualification burden is strategic and long-lived.
Supply-chain resilience
Internal AM may reduce lead time for tooling, spares, repair or obsolete components. The benefit is real only if feedstock, post-processing, inspection and approved data remain available during the disruption being mitigated.
When outsourcing is stronger
Demand is uncertain or intermittent
Service providers can aggregate demand across customers and technologies. This avoids carrying expensive underutilized equipment and specialist labor.
The process is highly specialized
Large-format DED, electron-beam PBF, reactive-metal production, high-resolution CT, HIP, advanced surface finishing and specialized furnace routes may be difficult to justify internally.
Speed to first part matters
An experienced supplier with qualified equipment and downstream operations can deliver useful evidence faster than a new internal team can install, stabilize and validate a production line.
Technology flexibility matters
Outsourcing allows an organization to compare LPBF, binder jetting, polymer PBF, DED and other routes without committing capital to one platform. This is valuable during application discovery.
External qualification already exists
A supplier may already hold customer approvals, material data, special-process accreditations and production experience that would take years to replicate.
The make-or-buy decision matrix
Decision factor
Favors insourcing
Favors outsourcing
Application demand
Stable, recurring and visible
Variable, early-stage or project-based
Strategic differentiation
Process knowledge or iteration creates competitive advantage
Part is non-core or commercially available
IP sensitivity
Geometry and parameters are highly sensitive
Controlled supplier exchange is acceptable
Technology breadth
One process family covers most needs
Applications require several technologies or materials
Qualification
Long-term program justifies internal qualification
Supplier holds relevant approvals and evidence
Lead time
Frequent urgent demand benefits from local control
Qualified supplier can deliver faster than capability build-up
Capital and utilization
High utilization and funded infrastructure
Low or uncertain utilization
Talent
Experienced multidisciplinary team can be retained
Critical expertise is unavailable internally
Post-processing
Required downstream operations are controlled internally
Supplier provides an integrated finished-part route
Supply risk
External capacity or geopolitical exposure is unacceptable
Multiple qualified suppliers provide resilience
Calculate total cost of ownership
The internal cost model should include more than equipment depreciation:
Facility preparation, utilities, inert gas and ventilation
Powder-safe or material-specific handling systems
Software licenses and computing infrastructure
Machine acceptance, calibration and maintenance
Engineering, operator and quality labor
Training and qualification
Feedstock inventory, testing and obsolescence
Build failures, rework and development builds
Heat treatment, machining, finishing and inspection
Data systems, cybersecurity and record retention
Downtime, spare parts and service contracts
Cost of underutilized capacity
The supplier quotation should also be normalized. Determine whether it includes design support, material, post-processing, inspection, documentation, shipping, non-recurring engineering and qualification. Compare cost per accepted finished part, not print-hour rate.
Utilization is necessary but not sufficient
High machine utilization can still destroy value if the portfolio consists of low-value parts or development work that never transitions to production. Track:
Productive versus experimental build hours
First-pass yield and accepted-part output
Post-processing queue and total lead time
Engineering hours per released part
Value created through performance, tooling avoidance or lead-time reduction
Percentage of applications reaching recurring production
Qualification ownership must be explicit
Outsourcing does not transfer engineering accountability automatically. The customer and supplier should define who owns:
Part design and DfAM decisions
Material and process specifications
Parameter approval and change control
Machine equivalency and site transfer
Heat-treatment and post-processing approval
Inspection technique and acceptance criteria
Nonconformance disposition
Data retention and audit access
ISO/ASTM 52901 provides a useful basis for defining the information exchanged between the purchaser and AM part provider, including part definition, feedstock, final characteristics, inspection and acceptance.
How to evaluate an AM supplier
Relevant experience: Has the supplier produced comparable geometry, alloy and criticality?
Process control: How are parameters, software, machine state and material lots controlled?
Downstream integration: Which post-processing and inspection steps are internal or subcontracted?
Quality evidence: What qualifications, accreditations, material data and historical yield exist?
Change management: What changes require customer notification or approval?
Capacity: What is the actual bottleneck at target volume?
Data and IP: Who owns build files, supports, parameters, monitoring data and improvement knowledge?
Business continuity: Are service, spare parts, secondary machines and backup sites available?
Transparency: Will the supplier share nonconformance, yield and root-cause information?
Exit plan: Can production be transferred if the supplier or platform becomes unavailable?
The hybrid model
A hybrid model often provides the best learning-to-risk ratio. Common configurations include:
Internal polymer printing and DfAM; external metal production
Internal prototype metal machine; qualified production at a supplier
Internal LPBF; external HIP, machining or CT
Internal application engineering and inspection; external build execution
Dual sourcing between an internal line and an external qualified partner
The interfaces must be explicit. A fragmented hybrid route can create more logistics and configuration risk than either full insourcing or an integrated supplier.
A staged decision process
Build a process-neutral application pipeline.
Outsource representative parts to establish real cost, quality and lead time.
Develop internal DfAM, sourcing and acceptance capability.
Identify the recurring bottleneck: supplier capacity, iteration speed, IP, cost or qualification.
Model internal utilization and complete infrastructure requirements.
Compare outsource, hybrid and insource scenarios over the program life.
Run a pilot capability with measurable transition criteria.
Scale only after accepted-part economics and organizational readiness are demonstrated.
Red flags before buying a machine
The business case depends on a single unqualified part.
Post-processing and inspection are described as future problems.
Utilization assumptions use maximum build hours rather than accepted-part demand.
No one owns material, parameter and configuration control.
The team lacks dedicated process and quality resources.
The selected machine is justified by demonstrations rather than requirements.
The cost model excludes development failures, downtime and labor.
There is no plan for software, machine or supplier obsolescence.
Conclusion
Insourcing is justified when AM capability is strategically important, the application pipeline is credible and the organization can control the complete production route. Outsourcing is stronger when demand is uncertain, technology breadth matters or qualified external capability already exists. A staged hybrid approach is often the safest path from experimentation to industrial production.
As the aerospace manufacturing industry continues to soar to new heights, it is clear that the sector is one of the most advanced and sophisticated commercial manufacturing systems in existence. It’s an industry that is constantly pushing the boundaries of technology to build highly complex, safety-critical structures and parts. But, despite this, the industry is still largely reliant on human skill and dexterity during assembly.
There have been efforts to introduce automation into aerospace manufacturing, but the uptake has been relatively low. This begs the question: why? Some may point to the size of the parts or the need for extreme accuracy. However, as with any complex issue, the problems are multifaceted. There are many contradictions and unsettled aspects still to be resolved, and there are no clear-cut answers to the automation conundrum.
One of the biggest challenges facing the aerospace industry when it comes to automation is the complexity of the manufacturing process. It is not just a matter of automating one task or process; rather, it involves automating multiple tasks that require a high degree of precision and accuracy. Additionally, the parts and structures being built in aerospace manufacturing are often incredibly complex, with intricate geometries and shapes that can be difficult to manufacture using traditional techniques.
Another challenge facing the aerospace industry when it comes to automation is the need for flexibility. Aerospace manufacturing is a highly dynamic industry, with constantly changing requirements and specifications. As a result, manufacturers need to be able to quickly adapt and change their manufacturing processes to meet new demands. This can be difficult to achieve with automated systems, which are often rigid and inflexible.
Furthermore, the cost of implementing automation in aerospace manufacturing can be prohibitively high. The technology required to automate many of the manufacturing processes in aerospace is often expensive, and the initial investment can be significant. This cost can be further exacerbated by the need for specialized personnel to operate and maintain the automated systems.
Despite these challenges, there are compelling reasons for the aerospace industry to pursue automation. One of the most significant benefits of automation is the potential to increase efficiency and reduce costs. Automated systems can work faster and with greater precision than human operators, which can result in shorter production times and lower defect rates.
Another potential benefit of automation in aerospace manufacturing is improved safety. Human error is a leading cause of accidents in the aerospace industry, and automation can help to reduce the risk of accidents by eliminating the need for human operators in dangerous or hazardous situations.
Finally, automation can help to address the skills gap in the aerospace industry. The industry is facing a shortage of skilled workers, and automation can help to mitigate this issue by reducing the need for highly skilled personnel in certain areas of the manufacturing process.
So, what needs to be done to increase the uptake of automation in aerospace manufacturing? One potential solution is to focus on developing more flexible and adaptable automated systems. This would allow manufacturers to quickly adapt their manufacturing processes to meet changing requirements and specifications, without having to invest in new systems or equipment.
Another solution is to focus on reducing the cost of implementing automation in aerospace manufacturing. This could involve developing more affordable technologies or finding ways to reduce the costs associated with operating and maintaining automated systems.
Ultimately, the key to increasing the uptake of automation in aerospace manufacturing is to continue to innovate and develop new technologies that can address the unique challenges facing the industry. By working together, industry stakeholders can help to build a more efficient, safer, and sustainable aerospace manufacturing sector that can meet the demands of tomorrow.
In conclusion, while the aerospace manufacturing industry is one of the most advanced and sophisticated commercial manufacturing systems in existence, there is still much work to be done when it comes to automation. The challenges facing the industry are multifaceted, and there are no clear-cut answers to the automation conundrum. However, with a continued focus on innovation and collaboration, the aerospace industry