Tag: Supply Chain

  • Casting vs Forging vs Additive Manufacturing: When Does AM Actually Remove the Bottleneck?

    Casting vs Forging vs Additive Manufacturing: When Does AM Actually Remove the Bottleneck?

    Additive manufacturing does not remove every aerospace bottleneck. Sometimes it removes tooling and long-lead forgings; sometimes it simply moves the constraint into powder, HIP, machining, CT/NDT or qualification. The right comparison is total program constraint, not printer cycle time.
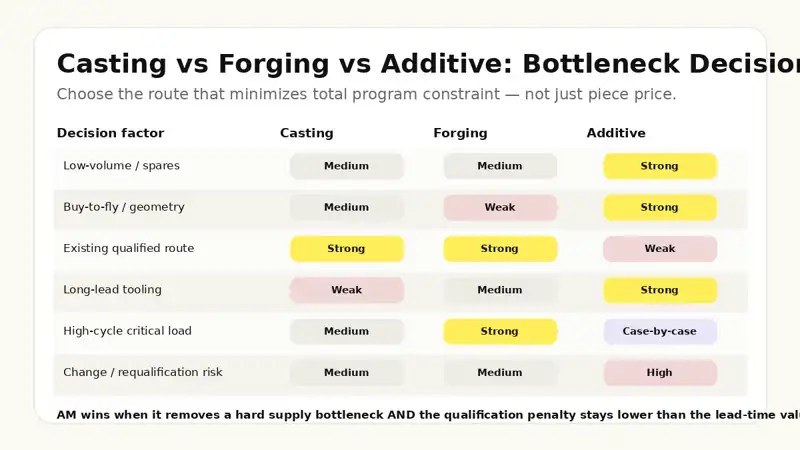
    Decision matrix comparing casting, forging and additive manufacturing across supply-chain and qualification factors.
    A practical decision map: AM is most valuable when it removes a hard supply bottleneck and the qualification penalty is smaller than the lead-time value created.

    Why this question matters in 2026

    Aerospace supply chains are still constrained by engines, electronics, castings, forgings, titanium and high-temperature alloys. Deloitte’s 2026 aerospace and defense outlook describes AM as a targeted resilience tool for low-volume, long-lead or hard-to-source parts—not as a universal replacement for conventional manufacturing.

    The constraint is visible in corporate actions, too. In September 2026, GE Aerospace announced an agreement to acquire Consolidated Precision Products, explicitly framing mission-critical casting capacity as necessary to support demand across commercial engines, aftermarket and defense. When an OEM is willing to spend billions to secure casting capacity, “just print it” is clearly not the default answer—but neither is “stay with the legacy route forever.”

    The bottleneck-removal test

    Before choosing AM, ask four questions in sequence:

    1. What is the actual constraint? Tooling? Raw material? Forge/foundry capacity? Buy-to-fly? Machining? Supplier minimum order quantity? Obsolescence?
    2. Can AM remove that constraint technically? Does the geometry, alloy, size and property requirement fit a mature process route?
    3. What new constraint does AM introduce? Powder/feedstock, build rate, support removal, HIP, heat treatment, machining, surface finish, CT/NDT, machine equivalence or qualification?
    4. Is the net program value positive? Compare avoided lead time and inventory against qualification, post-processing, yield and recurring cost.

    Casting vs forging vs additive: the decision matrix

    Part / program conditionCastingForgingAdditive
    High annual volume with stable geometryUsually strong once tooling/process are establishedStrong for load-critical shapes if capacity existsOften weak on unit economics unless geometry creates major value
    Low volume / spares / obsolescenceTooling and MOQ can hurtSmall lots can be difficultOften strong, especially with digital inventory
    Very high structural load / fatigue criticalityApplication-dependentOften preferred due to mature property pedigreePossible, but qualification and defect tolerance can dominate
    Complex internal flow pathsPossible but tooling/core complexity risesUsually poor fitStrong technical fit; inspectability may become the gate
    Extreme buy-to-fly ratioPotentially goodCan still require heavy machiningPotentially strong for expensive Ti/Ni alloys
    Long tooling lead timeWeak for urgent demandDies/tooling can constrain responseStrong if a qualified AM route already exists
    Existing mature qualified supply chainStrongStrongAM must overcome a qualification penalty to justify change
    Supplier capacity crisisMay be the bottleneckMay be the bottleneckCan be a resilience route if downstream AM capacity is actually available

    When AM genuinely removes the bottleneck

    1. Low-volume, long-lead hardware

    AM is strongest when tooling amortization is poor, demand is intermittent and carrying inventory is expensive. Legacy spares, defense sustainment hardware and space components often fit this pattern.

    2. Titanium or nickel parts with punitive buy-to-fly

    If the conventional route starts from a large billet or forging and machines most of it away, near-net AM can reduce raw-material exposure. That advantage is most valuable when alloy supply is constrained or scrap recovery does not fully compensate for long lead time.

    3. Tooling is the pacing item

    Investment-casting tooling, cores, forging dies and associated development loops can make the calendar inflexible. AM can collapse tooling time—but only if the AM process route is already mature enough to avoid replacing a tooling delay with a qualification delay.

    4. Part consolidation removes supplier interfaces

    A printed assembly that eliminates multiple details, welds, braze joints, fasteners or supplier handoffs may remove more schedule risk than its unit cost suggests. The value is system-level simplification.

    When AM only transfers the bottleneck

    • Powder/feedstock: a constrained or single-source alloy can recreate the same upstream dependency.
    • HIP and heat treatment: downstream special-process capacity may become the new queue.
    • Machining: AM rarely eliminates all machining for aerospace interfaces and critical surfaces.
    • CT/NDT: complex internal geometry can require expensive inspection with limited throughput.
    • Surface integrity: fatigue-critical parts may need substantial finishing and validation.
    • Qualification: the biggest trap is switching to AM to save six months of sourcing and then spending 18 months proving the new route.

    The qualification penalty

    The correct economic model should treat qualification like an up-front switching cost. A legacy casting or forging route may have terrible lead time but decades of accepted data. AM may have excellent responsiveness but require new material/process evidence, inspection substantiation, machine equivalence work and component-level testing.

    A simple decision rule is:

    Choose AM when the present value of avoided lead time, inventory, tooling, scrap and supply risk is greater than the qualification penalty plus the new recurring AM constraints.

    A five-case screen

    CaseLikely answerWhy
    Low-volume Ti bracket, heavy machining from billet, non-fracture-criticalAM candidateMaterial savings + no tooling + manageable evidence burden.
    High-volume rotating engine diskForging remains favoredExtreme property/defect-tolerance requirements and mature forged pedigree.
    Complex combustor or thermal-management featureAM can winGeometry creates functional value conventional processes struggle to achieve.
    Legacy casting with broken tooling and 18-month supplier lead timeAM worth screeningObsolescence and tooling avoidance can dominate if qualification scope is bounded.
    Simple commodity geometry with stable qualified forging supplyStay conventionalAM adds cost and qualification with little bottleneck value.

    The key procurement mistake

    Teams often compare the quoted AM part price with the quoted casting/forging price. That misses the point. The comparison should include calendar time, tooling cash, inventory, material yield, minimum order quantities, supplier concentration, engineering-change responsiveness, post-processing queues, inspection throughput and qualification cost.

    AM is not automatically cheaper. It can be economically superior because it changes the shape of the constraint.

    Sources & further reading

    This decision framework is directional. Flight-critical manufacturing-route changes require application-specific engineering, quality and regulatory review.
  • Insource or Outsource Additive Manufacturing? A Make-or-Buy Framework

    Insource or Outsource Additive Manufacturing? A Make-or-Buy Framework

    The decision to insource or outsource additive manufacturing is not simply a comparison between machine price and supplier quotation. It is a capability decision involving application pipeline, utilization, intellectual property, process ownership, qualification, post-processing, inspection and long-term supply risk.

    Buy a machine when owning the manufacturing capability creates durable strategic value. Buy parts when external capability delivers the required result with lower total risk.

    Three operating models

    ModelWhat remains internalBest fit
    OutsourceRequirements, design authority, supplier management and acceptanceEarly adoption, variable demand, specialized processes or limited internal expertise
    HybridApplication engineering, prototyping or selected builds; external production or post-processingOrganizations building knowledge while managing capital and qualification risk
    InsourceEquipment, operators, process control, production data and often post-processingStrategic IP, stable workload, rapid iteration, controlled qualification or supply-chain need

    Many successful programs move through these models over time. Outsourcing can be the fastest way to validate applications. A hybrid model can build internal design and process knowledge. Full insourcing becomes attractive only when the application portfolio, organization and downstream infrastructure are ready.

    The first question: what capability are you buying?

    An AM machine does not create an industrial capability by itself. A complete capability may require:

    • Application and DfAM engineering
    • Build preparation and process engineering
    • Feedstock storage, handling and traceability
    • Qualified equipment, software and parameters
    • Environmental, health and safety controls
    • Heat treatment, HIP, debinding or sintering
    • Support removal, machining and surface finishing
    • Cleaning, metrology, NDT and material testing
    • Quality systems, data retention and change control
    • Maintenance, service and spare-parts support

    If most of these remain external, the organization may be insourcing a printer while still outsourcing the production system.

    When insourcing is strategically attractive

    Rapid design–build–test loops

    Internal equipment can compress iteration cycles when engineers, operators and test teams work closely. This is valuable for R&D, tooling, repair development and products whose geometry changes frequently.

    Sensitive intellectual property

    Insourcing can reduce exposure of geometry, parameters and performance data. It does not remove cybersecurity risk; internal access, file transfer and machine networks still need control.

    Stable and repeatable demand

    A credible internal application pipeline improves equipment utilization and supports operator proficiency. The pipeline should be based on production-ready candidates rather than a long list of parts that are merely printable.

    Qualification ownership

    Some organizations need direct control of parameters, machine condition, material genealogy and production records. This can justify insourcing when the qualification burden is strategic and long-lived.

    Supply-chain resilience

    Internal AM may reduce lead time for tooling, spares, repair or obsolete components. The benefit is real only if feedstock, post-processing, inspection and approved data remain available during the disruption being mitigated.

    When outsourcing is stronger

    Demand is uncertain or intermittent

    Service providers can aggregate demand across customers and technologies. This avoids carrying expensive underutilized equipment and specialist labor.

    The process is highly specialized

    Large-format DED, electron-beam PBF, reactive-metal production, high-resolution CT, HIP, advanced surface finishing and specialized furnace routes may be difficult to justify internally.

    Speed to first part matters

    An experienced supplier with qualified equipment and downstream operations can deliver useful evidence faster than a new internal team can install, stabilize and validate a production line.

    Technology flexibility matters

    Outsourcing allows an organization to compare LPBF, binder jetting, polymer PBF, DED and other routes without committing capital to one platform. This is valuable during application discovery.

    External qualification already exists

    A supplier may already hold customer approvals, material data, special-process accreditations and production experience that would take years to replicate.

    The make-or-buy decision matrix

    Decision factorFavors insourcingFavors outsourcing
    Application demandStable, recurring and visibleVariable, early-stage or project-based
    Strategic differentiationProcess knowledge or iteration creates competitive advantagePart is non-core or commercially available
    IP sensitivityGeometry and parameters are highly sensitiveControlled supplier exchange is acceptable
    Technology breadthOne process family covers most needsApplications require several technologies or materials
    QualificationLong-term program justifies internal qualificationSupplier holds relevant approvals and evidence
    Lead timeFrequent urgent demand benefits from local controlQualified supplier can deliver faster than capability build-up
    Capital and utilizationHigh utilization and funded infrastructureLow or uncertain utilization
    TalentExperienced multidisciplinary team can be retainedCritical expertise is unavailable internally
    Post-processingRequired downstream operations are controlled internallySupplier provides an integrated finished-part route
    Supply riskExternal capacity or geopolitical exposure is unacceptableMultiple qualified suppliers provide resilience

    Calculate total cost of ownership

    The internal cost model should include more than equipment depreciation:

    • Facility preparation, utilities, inert gas and ventilation
    • Powder-safe or material-specific handling systems
    • Software licenses and computing infrastructure
    • Machine acceptance, calibration and maintenance
    • Engineering, operator and quality labor
    • Training and qualification
    • Feedstock inventory, testing and obsolescence
    • Build failures, rework and development builds
    • Heat treatment, machining, finishing and inspection
    • Data systems, cybersecurity and record retention
    • Downtime, spare parts and service contracts
    • Cost of underutilized capacity

    The supplier quotation should also be normalized. Determine whether it includes design support, material, post-processing, inspection, documentation, shipping, non-recurring engineering and qualification. Compare cost per accepted finished part, not print-hour rate.

    Utilization is necessary but not sufficient

    High machine utilization can still destroy value if the portfolio consists of low-value parts or development work that never transitions to production. Track:

    • Productive versus experimental build hours
    • First-pass yield and accepted-part output
    • Post-processing queue and total lead time
    • Engineering hours per released part
    • Value created through performance, tooling avoidance or lead-time reduction
    • Percentage of applications reaching recurring production

    Qualification ownership must be explicit

    Outsourcing does not transfer engineering accountability automatically. The customer and supplier should define who owns:

    • Part design and DfAM decisions
    • Material and process specifications
    • Parameter approval and change control
    • Machine equivalency and site transfer
    • Heat-treatment and post-processing approval
    • Inspection technique and acceptance criteria
    • Nonconformance disposition
    • Data retention and audit access

    ISO/ASTM 52901 provides a useful basis for defining the information exchanged between the purchaser and AM part provider, including part definition, feedstock, final characteristics, inspection and acceptance.

    How to evaluate an AM supplier

    1. Relevant experience: Has the supplier produced comparable geometry, alloy and criticality?
    2. Process control: How are parameters, software, machine state and material lots controlled?
    3. Downstream integration: Which post-processing and inspection steps are internal or subcontracted?
    4. Quality evidence: What qualifications, accreditations, material data and historical yield exist?
    5. Change management: What changes require customer notification or approval?
    6. Capacity: What is the actual bottleneck at target volume?
    7. Data and IP: Who owns build files, supports, parameters, monitoring data and improvement knowledge?
    8. Business continuity: Are service, spare parts, secondary machines and backup sites available?
    9. Transparency: Will the supplier share nonconformance, yield and root-cause information?
    10. Exit plan: Can production be transferred if the supplier or platform becomes unavailable?

    The hybrid model

    A hybrid model often provides the best learning-to-risk ratio. Common configurations include:

    • Internal polymer printing and DfAM; external metal production
    • Internal prototype metal machine; qualified production at a supplier
    • Internal LPBF; external HIP, machining or CT
    • Internal application engineering and inspection; external build execution
    • Dual sourcing between an internal line and an external qualified partner

    The interfaces must be explicit. A fragmented hybrid route can create more logistics and configuration risk than either full insourcing or an integrated supplier.

    A staged decision process

    1. Build a process-neutral application pipeline.
    2. Outsource representative parts to establish real cost, quality and lead time.
    3. Develop internal DfAM, sourcing and acceptance capability.
    4. Identify the recurring bottleneck: supplier capacity, iteration speed, IP, cost or qualification.
    5. Model internal utilization and complete infrastructure requirements.
    6. Compare outsource, hybrid and insource scenarios over the program life.
    7. Run a pilot capability with measurable transition criteria.
    8. Scale only after accepted-part economics and organizational readiness are demonstrated.

    Red flags before buying a machine

    • The business case depends on a single unqualified part.
    • Post-processing and inspection are described as future problems.
    • Utilization assumptions use maximum build hours rather than accepted-part demand.
    • No one owns material, parameter and configuration control.
    • The team lacks dedicated process and quality resources.
    • The selected machine is justified by demonstrations rather than requirements.
    • The cost model excludes development failures, downtime and labor.
    • There is no plan for software, machine or supplier obsolescence.

    Conclusion

    Insourcing is justified when AM capability is strategically important, the application pipeline is credible and the organization can control the complete production route. Outsourcing is stronger when demand is uncertain, technology breadth matters or qualified external capability already exists. A staged hybrid approach is often the safest path from experimentation to industrial production.

    Related Addithive resources: Industrial AM Workflow · Metal AM Supply Chain Map

    References and further reading

  • Additive Manufacturing: Redefining Mobility Production at Point of Use

    Additive Manufacturing: Redefining Mobility Production at Point of Use

    Additive Manufacturing, or 3D-printing, technology has been a significant advancement in the manufacturing industry, with one of its most frequently mentioned benefits being the ability to produce parts at the point of use. This technology allows for the downloading of a digital file and the creation of the part on-site, which has the potential to greatly compress supply chains, lead times, inventories, and design iterations for custom parts.

    The mobility industry, including automobile, aerospace, and transportation sectors, is one that demands precision, high-quality, and cost-effective solutions. Additive Manufacturing technology, with its ability to create complex geometries, lightweight designs, and rapid prototyping, is uniquely suited to meet the demands of the mobility industry. However, the viability of this technology for production at the point of use is not universal and depends on several factors, such as size, materials, build time, manufacturing complexity, cost, and competing technologies.

    For the mobility industry, one of the key challenges is the size of the parts that can be produced using Additive Manufacturing technology. This is due to the limited build volume of the printer, which can increase the build time and cost for larger parts. Additionally, the quality of the part may be compromised due to the limitations of the printing process, which may not be suitable for high-stress applications, such as those found in the mobility industry.

    Another challenge for the mobility industry is the limited range of materials that can be used for Additive Manufacturing. Although the range of materials that can be used has expanded with advancements in materials science, the majority of Additive Manufacturing materials are limited to plastics and some metals. This may not be suitable for applications that require high-strength materials, such as those found in the aerospace or automotive industries.

    Despite these challenges, the mobility industry is investing in Additive Manufacturing capacity for production at the point of use. One of the key benefits of this technology is the ability to reduce supply chain and inventory costs by producing parts on-site. Additionally, the ability to create complex geometries and lightweight designs can lead to a reduction in fuel consumption and emissions, which is crucial in the transportation industry.

    Moreover, Additive Manufacturing technology can significantly reduce the design iterations required for custom parts, leading to a faster time-to-market for new products and an increase in the speed of innovation. For instance, automotive companies can use Additive Manufacturing technology to rapidly prototype and test new designs, which can reduce the time and cost associated with traditional manufacturing methods.

    However, it is essential for companies in the mobility industry to evaluate the feasibility and benefits of Additive Manufacturing technology on a case-by-case basis. This requires a deep understanding of the technology and its capabilities, as well as an evaluation of the costs and benefits associated with using Additive Manufacturing technology for production at the point of use.

    In conclusion, Additive Manufacturing technology is a significant advancement for the mobility industry, providing unique advantages such as the ability to produce parts at the point of use and reduce supply chain and inventory costs. However, the viability of this technology for production at the point of use is dependent on several factors, including the size and complexity of the part, the materials used, and the cost of the technology. Therefore, it is important for the mobility industry to carefully evaluate the feasibility and benefits of Additive Manufacturing technology for their specific needs.