Updated 12 September 2026. This revision replaces the earlier 2022–2025 narrative with a source-linked production assessment.
Metal binder jetting selectively deposits a binder into a powder bed to form a fragile green part. The subsequent thermal route consolidates the metal. Its commercial potential depends on handling yield, sintering control and accepted-part cost as much as printing speed.
What has become commercially concrete?
HP offers Metal Jet configurations covering development and production, with curing, powder handling and furnace operations forming part of the workflow. This is evidence of an offered industrial platform, not proof of profitability for every application. HP Metal Jet configurations and workflow.
Binder jetting vs LPBF: compare the whole route
Decision factor
Metal binder jetting
Metal LPBF
Consolidation
Binder forms the green shape; sintering consolidates metal later.
Metal melts and solidifies during printing.
Geometry constraints
Green-part strength, depowdering access, shrinkage and sintering distortion.
Supports, thermal distortion, recoater clearance and powder escape.
Production constraint
Curing, handling, furnace loading and sintered-part yield may limit output.
Build time, powder handling and downstream operations may limit output.
Finished-part evidence
Density, chemistry, dimensional capability and properties after the full thermal route.
Properties after the specified build, thermal and finishing route.
Commercial comparison
Compare total accepted-part cost against MIM, machining and casting.
Compare total accepted-part cost and system-level design benefit.
Five gates before calling an application production-ready
1. Material: qualify the actual powder, binder and thermal combination. A material demonstration is not universal alloy availability.
2. Handling: measure breakage during green-part extraction, transfer and loading. Printing without attached supports does not eliminate handling fixtures or sintering setters.
3. Sintering: validate shrinkage compensation, distortion, carbon and oxygen control, density and furnace load consistency across representative geometries.
4. Part release: establish dimensional inspection, surface condition, defect acceptance and mechanical-property evidence appropriate to the application.
5. Economics: include labor, fixtures, furnace occupancy, machining, inspection, scrap and qualification costs. Avoid universal claims about speed, energy savings or break-even volume.
Use accepted parts as the economic denominator
For a defined production batch, divide all allocated production and quality costs by the number of released, conforming parts. Compare alternatives using the same geometry, annual volume and acceptance criteria. A faster print stage can simply move the queue to the furnace.
Grade-specific qualification, repeat powder purchases and economically meaningful revenue exposure.
Technical sources: HP Metal Jet and Carpenter Additive. The powder-supplier example is a supply-chain research candidate; it does not establish a supplier relationship for a particular HP installation.
Company exposure is a research starting point, not a stock recommendation. A relevant technology does not establish material revenue, attractive margins or a reasonable valuation. Check current filings, ownership, cash flow and customer concentration before drawing an investment conclusion.
What would change the assessment?
Stronger evidence would include named repeat-production applications, measured yield across multiple furnace loads, independent property data for the specified route and orders converted into cash. A demonstration part or announced capacity alone is weaker evidence.
Assess binder jetting through the full production route. The Industrial AM Bottleneck Atlas 2026 connects manufacturing constraints with qualification, economics and company exposure.
Binder jetting selectively deposits a liquid binder onto a powder bed to create a “green” part. The printing step is relatively fast and does not use a laser to melt each voxel. But for metal and many ceramic applications, printing is only the beginning: curing, depowdering, debinding and sintering determine the final geometry and properties.
The central binder-jetting challenge is not print speed. It is controlling the complete print-to-sinter route with acceptable shrinkage, distortion, density and yield.
How binder jetting works
A recoater spreads a controlled layer of powder.
An inkjet printhead selectively deposits binder according to the sliced geometry.
The build platform moves and the process repeats.
The powder bed is cured or dried to provide handling strength.
Green parts are removed from the surrounding powder and cleaned.
For metal or ceramic routes, the binder is removed and the part is sintered.
Finishing, heat treatment, machining and inspection are applied as required.
Sand molds and cores follow a different downstream route: the printed sand tool is cleaned and used directly in a casting process rather than sintered into a dense metal component.
Three distinct binder-jetting markets
Application
Printed material
What the printed object becomes
Main value driver
Metal binder jetting
Metal powder plus binder
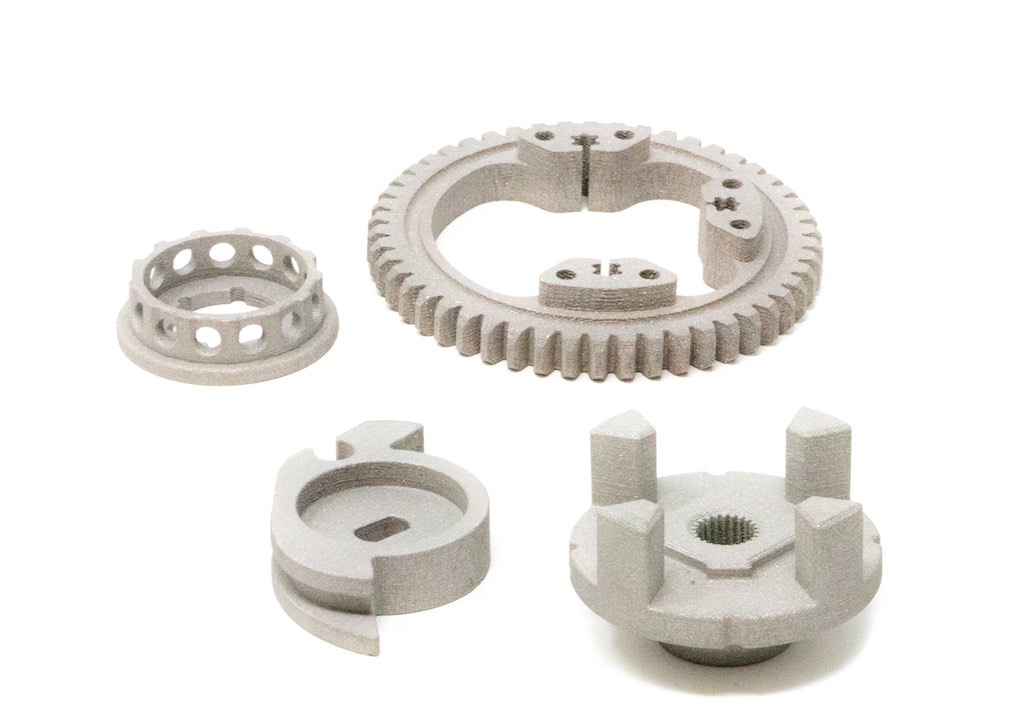
A sintered metal component
Batch productivity, geometry, use of powder-metallurgy feedstocks
Sand binder jetting
Foundry sand plus binder
A mold or core for casting
Toolless complex casting geometry and short lead time
Ceramic binder jetting
Ceramic powder plus binder
A fired or sintered ceramic component
Material flexibility and complex refractory or technical-ceramic shapes
Why metal binder jetting is attractive
High packing density: parts can often be nested in three dimensions because attached thermal supports are not required during printing.
Area-wide deposition: print time is less sensitive to the number of individual parts than point-scanning laser processes.
Powder-metallurgy compatibility: many systems use powders and sintering knowledge related to MIM or conventional powder metallurgy.
Lower thermal stress during printing: the green part is not locally melted by a high-energy beam.
Potential production economics: the process can be competitive for suitable small-to-medium parts when printing, furnace loading and yield are balanced.
These advantages are conditional. If depowdering is difficult, green parts break, sintering distorts the geometry or furnace capacity is constrained, the apparent print-speed advantage disappears.
The manufacturing bottlenecks
Green-part strength
Freshly printed parts are fragile. Binder saturation, drying, powder packing and geometry determine whether a component survives excavation, cleaning and transfer. Thin walls, long unsupported features and handling points need special attention.
Depowdering
Internal channels and densely nested builds can trap powder. The design must provide access for gravity, air, vibration, vacuum or automated cleaning. Powder removal must not damage green surfaces or contaminate subsequent batches.
Debinding
Binder removal must avoid cracking, blistering or carbon contamination. Thick sections and nonuniform geometry can produce internal pressure or differential debinding rates. The binder chemistry, heating cycle and atmosphere form part of the qualified process.
Sintering shrinkage
Metal binder-jetted parts shrink substantially as porosity is removed during sintering. The design is scaled before printing, but shrinkage is not always perfectly uniform. Geometry, powder packing, gravity, friction with setters, furnace temperature uniformity and local section thickness all influence final dimensions.
Distortion and support in the furnace
A part may print without supports yet still require setters, sintering supports or sacrificial features. At high temperature the component can creep under its own weight. Unsupported spans, asymmetric mass and thin walls are vulnerable.
Furnace capacity
The printer can produce green parts faster than downstream furnaces can process them. Furnace cycle time, usable hot-zone volume, atmosphere, loading strategy and material changeover often determine plant throughput.
Design for metal binder jetting
Use wall thicknesses and aspect ratios demonstrated for the specific powder and process.
Avoid large abrupt changes in section thickness that debind and sinter at different rates.
Provide powder-removal access to internal volumes.
Use generous radii and smooth transitions to reduce stress concentration during handling and sintering.
Orient broad surfaces and long spans to minimize gravity-driven distortion.
Plan setters or sintering supports before freezing the geometry.
Add machining stock to precision interfaces.
Separate cosmetic, dimensional and structural requirements by surface.
Design witness features or coupons when they provide meaningful process evidence.
Material properties: compare the qualified route
Density, strength, ductility, fatigue and corrosion performance depend on powder chemistry, particle-size distribution, binder, printing parameters, debinding, sintering atmosphere and thermal cycle. Published “fully dense” claims should be reviewed with the actual density method, test orientation, specimen geometry and material condition.
Metal binder jetting can produce strong and useful components, but it should not be assumed equivalent to wrought, MIM or LPBF material without application-specific data. Fatigue-sensitive and safety-critical uses require particular attention to residual porosity, inclusions, surface condition and dimensional variation.
Binder jetting versus LPBF
Factor
Metal binder jetting
Metal LPBF
During printing
Binder joins powder; no local melting
Laser creates a local melt pool
Thermal supports
Not attached during printing
Often required for anchoring and heat transfer
Primary thermal challenge
Debinding and sintering shrinkage/distortion
Residual stress, distortion and cracking during/after build
Part nesting
Three-dimensional nesting can be possible
Usually arranged from the build plate with support constraints
Surface/detail
Process and powder dependent; sintering affects final geometry
Generally finer control for qualified compact features, but downskin remains challenging
Post-processing
Cure, depowder, debind, sinter; machining/finishing as required
Depowder, stress relief, cut-off, support removal; machining/finishing as required
Strongest economic case
Batch production of suitable sinterable geometries
High-value complex parts, internal channels and qualified performance
Current industrial platform landscape
The supplier landscape has consolidated and evolved since the early binder-jetting boom. Product names and corporate ownership should be checked at the time of procurement. As of 2026, notable active examples include:
Desktop Metal: the X-Series family includes InnoventX, X25Pro and X160Pro for metals, ceramics and composites; the Shop System targets batch metal production. ExOne technology and sand systems are presented within the broader Desktop Metal portfolio.
HP: the Metal Jet S100 platform is offered in development and production configurations, with expanded materials and powder-management options announced in 2026.
voxeljet: continues to offer large-format binder-jet systems for sand molds, cores and other powder materials.
Ricoh: continues development of aluminum metal binder jetting, with emphasis on thermal applications and industrialization.
A machine list is not a technology assessment. Buyers should evaluate local service, installed-base experience, material availability, furnace integration, application references, software, yield and long-term support.
Questions to ask before selecting a binder-jet route
What is the complete print, cure, depowder, debind and sinter cycle for this material?
What shrinkage and dimensional capability have been demonstrated on comparable geometries?
Which features require setters, sintering supports or machining?
What green-part breakage and sintering scrap rates are typical?
What limits furnace loading density and cycle time?
How are powder batches, binder condition and reused powder controlled?
Which material properties are based on production-representative parts rather than ideal test coupons?
How is residual powder verified in internal channels?
What is the inspection plan for porosity, distortion and critical dimensions?
What is the cost per accepted part at the target annual volume?
Standards direction
ISO/ASTM is developing a dedicated binder-jetting design guideline for single-alloy metal parts using multi-step binder jetting. The work reflects the need to standardize design principles around green-part behavior, depowdering, debinding and sintering rather than treating binder jetting as a simple support-free printing process.
Conclusion
Binder jetting is a compelling production route when part geometry, batch density and sintering behavior align. Its economics cannot be judged from printer speed alone. The winning production system balances print capacity with depowdering, green-part handling, furnace throughput, dimensional compensation, finishing and quality assurance.
This article originally described Carbon, Desktop Metal, Formlabs, Xometry and Velo3D as five disruptive additive manufacturing startups. The framing is no longer reliable as a current market guide.
The list mixed private companies, public companies, manufacturing marketplaces and equipment providers at very different stages of maturity. Ownership, financial condition, product strategy and public-market status have also changed since publication.
A private production-platform company whose product, material and customer position should be evaluated from current company and customer evidence
Desktop Metal
Its ownership and operating status changed materially after the 2023 article
Formlabs
A mature private AM platform company rather than an early-stage startup in the ordinary sense
Xometry
A public digital-manufacturing marketplace with AM as one of several production processes
Velo3D
A public metal-AM equipment company whose investment case depends on current revenue, cash, margins and installed-base execution
For example, Nano Dimension completed its acquisition of Desktop Metal in April 2025. Nano Dimension later reported Desktop Metal in discontinued operations following bankruptcy and deconsolidation. This illustrates why old company lists should not remain positioned as evergreen market research.
How Addithive evaluates companies now
AM exposure: how much of the business genuinely depends on additive manufacturing
Value-chain position: equipment, materials, software, services, post-processing or end-user adoption
Bottleneck ownership: whether the company controls a constraint required for AM to scale
Commercial proof: repeat orders, qualified production and customer concentration
Economics: gross margin, cash burn, recurring revenue and capital intensity
Platform durability: service network, installed base, material ecosystem and switching costs
Ownership and investability: public listing, parent-company exposure and transaction risk
Valuation and downside: the difference between a strong technology and an attractive security
Archive status: This URL is retained for historical reference and existing external links. It is not a current startup ranking, recommendation or investment list.
Desktop Metal, in partnership with Sandvik Additive Manufacturing and a top five global automaker, has announced that copper alloy C18150, also known as chromium zirconium copper, has been DM Qualified for binder jet 3D printing on the Production System. This material is commonly used in electrical and electronic components due to its high-strength and high-conductivity properties. The automaker is testing a unique 3D printed part design, which is being developed for a future production application, in C18150 using Sandvik’s Osprey metal powder. The companies will discuss details of this joint automotive project during a presentation at AMUG 2023 in Chicago. With the addition of C18150, Desktop Metal now offers a world-leading 23 metal materials on its binder jet 3D printing systems, including the Shop System, Production System, and X-Series platforms.
Chromium zirconium copper offers a combination of strength, conductivity, and corrosion resistance that makes it suitable for a wide range of industrial and commercial applications. The material has now been qualified for use on the high-speed Printing System platform in collaboration with Sandvik Additive Manufacturing, who provided C18150 powder that routinely delivered as-sintered densities of 98-99% when printed on the P-1. The automaker will scale a part design in C18150 for serial production on the Production System P-50 after additional development.
Chromium zirconium copper parts via Desktop Metal
Desktop Metal’s founder and CEO, Ric Fulop, expressed pride in announcing the qualification of chromium zirconium copper as a qualified material, bringing the company’s world-leading portfolio of binder jet materials to 23 metals. He also highlighted the simultaneous announcement of 304L qualification on the Shop System and Ti64 customer-qualification on the Production System. The company’s experts are collaborating with customers on application-specific material and part qualification projects for future Additive Manufacturing 2.0 production.
Desktop Metal Production System
Desktop Metal’s binder jet technology can 3D print almost any powder. The company has a tiered material qualification system for metals to signify the varying levels of material property results produced by its technology. DM Qualified signifies printing and sintering profiles developed by DM, with fully characterized material and mechanical properties that meet MPIF or other similar standards where available. Customer-Qualified materials have been qualified by customers with their own standards and are being successfully printed for their own applications. R&D Materials signify initial testing completed by DM demonstrating binder and process compatibility, with printing and sintering profiles under final development.
The Production System platform features high-speed Single Pass Jetting (SPJ) technology on two models: the P-1, for research and development of binder jetting projects for serial production, and the P-50, the world’s fastest metal binder jet system, offering the lowest cost per part, with SPJ technology. With C18150 qualification, the Production System now offers a wider range of options for customers seeking to use copper alloys in their products.
Desktop Metal and Sandvik will provide an update on binder jetting of Ti64 and Al6061 at AMUG 2023. The companies will also discuss details of the automotive project during a panel discussion from 1:30-2:30 p.m. on Thursday, March 23, in the Joliet Room at the Hilton Chicago.
In conclusion, Desktop Metal’s qualification of copper alloy C18150 for binder jet 3D printing on the Production System, in collaboration with Sandvik Additive Manufacturing and a top five global automaker, represents a significant milestone in the company’s efforts to provide a world-leading portfolio of binder jet materials to its customers. The partnership has demonstrated the capabilities of binder jetting in the production of complex parts in copper alloys, opening up a range of applications in thermal transfer and other
TriTech Titanium Parts LLC, a Detroit-based manufacturer of titanium parts for aerospace, marine, and automotive industries, and Desktop Metal, Inc., a global leader in additive manufacturing technologies for mass production, have announced the customer-qualification of Ti64 for binder jet 3D printing on the Production System™. The high-speed Single Pass Jetting (SPJ) technology platform features two models: the P-1, for research and development of binder jetting projects for serial production, and the P-50, the world’s fastest metal binder jet system, offering the lowest cost per part with SPJ technology. Ti64 is a popular material, known for its excellent strength-to-weight ratio, corrosion resistance, and biocompatibility. Binder jetting of Ti64 simplifies the production of complex titanium parts, which can be challenging and expensive to fabricate using traditional manufacturing methods.
Desktop Metal Production System via Desktop Metal
TriTech Titanium Parts LLC, which is ISO 9001:2015 certified, uses metal injection molding (MIM), investment casting, and now binder jet 3D printing on the Desktop Metal Production System P-1 to produce titanium parts. The company is a spin-off of AmeriTi Manufacturing Co., which was founded in 1984 and sold last year to Kymera International.
TriTech’s owner, Robert Swenson, who is also the former owner of AmeriTi, stated that with binder jet 3D printing, titanium production of even the most complex geometries can be greatly simplified and achieved at a lower cost. Swenson, a graduate of Purdue University with a degree in Metallurgical Engineering and an MBA from Harvard Business School, is incredibly proud to be the first Desktop Metal Production System P-1 customer worldwide to binder jet 3D print titanium, and the company is excited to offer this new manufacturing technology to its customers.
With the latest addition to the material portfolio, Desktop Metal offers the ability to binder jet 23 metals, including copper, aluminum, and now, titanium. Ric Fulop, Founder and CEO of Desktop Metal, stated that they are excited to help engineers and manufacturers produce complex, once-impossible designs in a wide range of metals, including challenging materials such as titanium.
While Ti64 is a popular material, it’s also known for being expensive to manufacture. The material’s strength, as well as its low thermal conductivity and ductility, make it challenging to machine or produce with traditional manufacturing methods. Shaping the material with MIM requires special knowledge and processes. TriTech is among a very small percentage of companies that produce titanium parts with MIM, and the company has developed its own MIM processes after years of R&D. However, with binder jetting, the process can be simplified and made more economical.
Binder jetting is a process where an industrial printhead selectively deposits a binder into a bed of Ti64 powder particles, creating a solid part one thin layer at a time, just like printing on sheets of paper. The form or shape produced by the printer is then sintered to high density and accuracy in a furnace, similar to the MIM process. Additionally, binder jetting allows unbound material to be reused in the process, adding to its cost efficiency.
Desktop Metal’s binder jet technology can 3D print almost any powder, which is why the company has a tiered material qualification system for metals to signify the varying levels of material property results produced by. Production System users interested in working with titanium should consult their Desktop Metal sales representative on hardware and binder requirements.
TriTech will discuss its experience binder jetting Ti64 at AMUG 2023, held March 19-23 in Chicago. The topic will be part of a Desktop Metal panel discussion from 1:30-2:30 p.m. Thursday, March 23,
Desktop Metal and CETIM have announced the successful qualification of 304L stainless steel for use on the Shop System™. This new development complements the suite of stainless steel materials already qualified on the mid-sized binder jet printer, including 17-4PH and 316L.
304L stainless steel is noteworthy for its high tensile strength, corrosion resistance, and durability, making it ideal for a wide range of applications, such as structural components, food processing equipment, fluid transfer components, and welded components. This new qualification means that it is now possible to produce complex geometries of 304L parts on demand with little to no waste, whether in low or high volumes.
Desktop Metal Shop System via Desktop Metal
CETIM, in collaboration with Desktop Metal, worked on the parameter development for 304L, enabling the material to be offered on the Shop System binder jet 3D printing system. The aim of this collaboration is to support quick production of critical replacement parts in the French energy sector, such as those used in fuel processing and nuclear components. This will help to reduce lead times for critical 304L maintenance parts, avoiding long and expensive downtimes in the factory.
Christophe Reynaud, Ph.D., Additive Manufacturing Material Engineer at CETIM, stated that “304L is a key material in the energy sector due to its corrosion resistance, suited for highly demanding environments such as civil nuclear applications. Coupled with the high versatility and responsiveness of the Shop System, it is now possible to considerably reduce the lead-time for critical 304L maintenance parts.”
This qualification of 304L stainless steel adds to the Shop System material portfolio, which now includes 17-4PH and 316L, IN625, and Cobalt-Chrome. IN718 is now fast-tracked for final development on Shop.
Ric Fulop, Founder and CEO of Desktop Metal, said, “This new material offering will allow manufacturers to produce complex geometries of 304L parts on demand with little to no waste, whether they are interested in low or high volumes. 304L is a flexible, widely used stainless steel across many industries, and we’re delighted to offer it in our affordable, popular Shop System model.”
The 304L stainless steel printed with the Shop System and sintered in an Ipsen graphite furnace meets or exceeds the minimum tensile properties and the chemical composition outlined in the ASTM A240 standard. Further development is underway to further qualify binder jet 3D printed 304L for use in food-processing equipment applications and for applications involving welding.
Desktop Metal Shop System Part via Desktop Metal
CETIM works closely with industrial companies to help identify market opportunities and facilitate innovation and technical progress. They were one of the first adopters of the Shop System, the Production System™ P-1, and also own a Desktop Metal Studio System™, a Bound Metal Deposition (BMD) metal printing system.
In conclusion, the qualification of 304L stainless steel for use on the Shop System™ is a significant development for the additive manufacturing industry. This new material offering will enable manufacturers to produce complex geometries of 304L parts on demand, with little to no waste, whether in low or high volumes. The collaboration between Desktop Metal and CETIM has made it possible to reduce lead times for critical 304L maintenance parts, avoiding long and expensive downtimes in the factory. The addition of 304L to the Shop System material portfolio complements the suite of stainless steel materials already qualified, including 17-4PH and 316L, IN625, and Cobalt-Chrome, making the Shop System an affordable, popular option for manufacturers across many industries.
Desktop Metal has announced the launch of Live Suite, a software package that simplifies the 3D printing process for metal, polymer, and ceramic parts. Live Suite builds on the success of the company’s Live Sinter™ simulation software, allowing users to bring their digital design data to life with ease and precision.
Utilizing advanced multi-physics simulation technology based on state-of-the-art GPUs, Live Sinter generates new design shapes that will produce the desired final part within tight tolerances. The software applies machine learning to calibrate the simulation process and match real-world results for the world’s largest binder jet system install base.
According to Ric Fulop, founder and CEO of Desktop Metal, “AM 2.0 is a digital manufacturing process that is ultimately powered by software, and we believe Live Suite offers the most intuitive and powerful AM software on the market.”
Desktop Metal’s Live Suite End-to-End Software Hub
Live Suite eliminates the need for users to purchase expensive 3D printing software programs to operate their equipment. The platform is designed to keep digital manufacturing accessible, so users have the tools they need and do not pay for expensive features they don’t require.
The Live Platform is a cloud-based hub for all Live Suite applications and services, organized into four content categories: build, manage, learn, and support. It allows users to manage their entire workflow in one location with 2FA security.
Live Platform is also the central administration hub for Live Suite, with the ability to provision and manage Desktop Metal 3D printing systems and users, as well as access firmware updates, knowledge, and technical support. The new Business Units feature allows larger companies with multiple users and departments to easily manage 3D printer permissions and controls for groups.
Live Suite includes a range of application-specific options, such as part serialization or optimized build instructions for specific parts ranging from dentures to valves. Special add-on features include Autopilot, which automates build preparation, and Live Monitor, which will soon be available to remotely view jobs as they progress through printers and ancillary equipment.
Live Suite offers several tools, including Live Sinter™, Live Build™ MFG, Live Build™ DLP, and Live Studio™. Live Sinter simplifies the production of sintered metal parts via binder jetting with powerful, generative AI multi-physics sintering simulation and new, scan-based adjustments that deliver parts with tight tolerances. Live Build MFG supports build preparation for all binder jet 3D printing of metal, wood, ceramic, and sand designs, while Live Build DLP is desktop-based build preparation software for customers of Desktop Health and ETEC digital light processing printers. Live Studio supports slicing and build preparation for Desktop Metal’s Bound Metal Deposition™ systems, including the Studio System 2.
Existing Desktop Metal equipment users will receive software updates starting today or by the end of the year. A schedule of the Live Suite rollout is available in the release notes, located in the Knowledge Base. Customers can also watch a Get Started video in the Academy.
Desktop Metal’s Live Suite is a game-changer for the additive manufacturing industry. By offering an integrated suite of applications and services, it streamlines the entire workflow, making it easier for users to manage their entire digital manufacturing process in one place. Moreover, with the incorporation of advanced multi-physics simulation and machine learning techniques, Live Sinter™ and Live Build™ simplify the 3D printing process and provide users with accurate and high-quality results. The cloud-based Live Platform™, with its centralized administration hub, provides users with 2FA security, and the ability to remotely manage and monitor their 3D printing systems and users, as well as access knowledge and technical support. This not only saves time and increases productivity but also eliminates the need to purchase other expensive 3D printing software programs. The wide range of add-on options available through Live Platform, including Autopilot and Live Monitor, further enhance the value proposition for users. In short, the Live Suite is a powerful and intuitive software suite that makes AM technology easy to use, cost-effective, and accessible to everyone.